Precision at Pace
sales@metalexuae.comHardened materials, intricate profiles and geometries conventional tools can't reach.
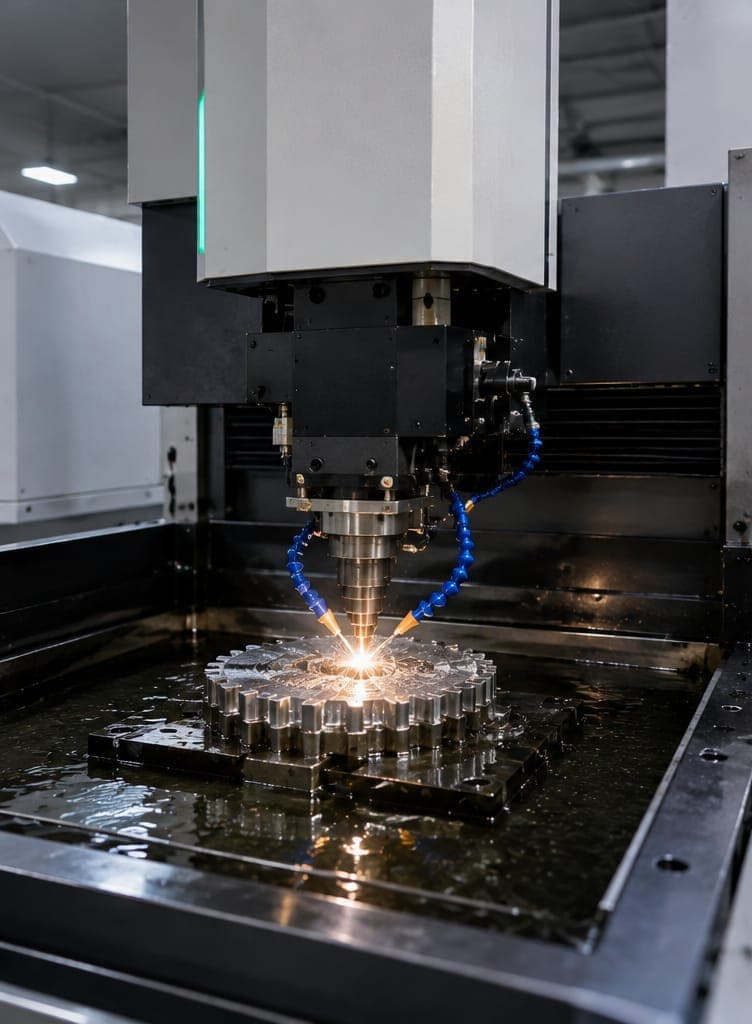
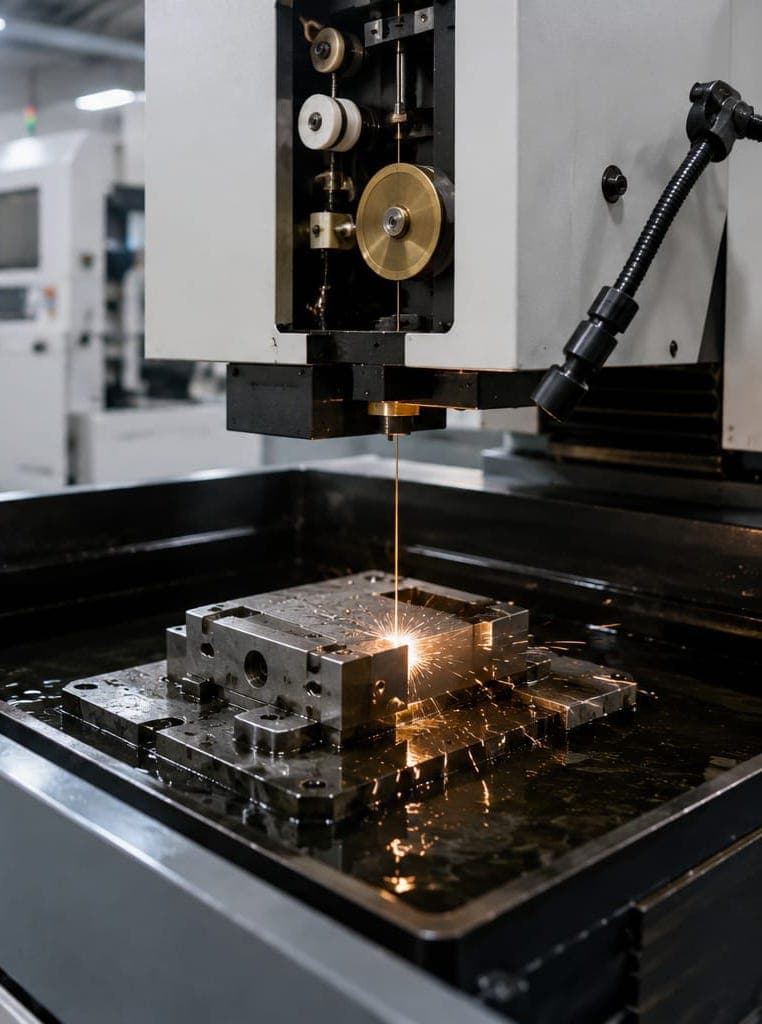
Electrical Discharge Machining removes material with precisely controlled electrical sparks rather than cutting force, which makes it the process of choice for hardened materials, intricate profiles and complex geometries where conventional machining is not feasible. METALEC operates both wire EDM and spark (sinker) EDM alongside its milling and grinding capacity.
Wire EDM cuts with a travelling wire electrode, producing sharp internal corners, fine slots, splines and interlocking profiles with excellent accuracy — straight through hardened tool steel. Spark EDM sinks shaped electrodes into the workpiece to create blind cavities, deep ribs and fine textures that no rotating cutter could reach.
Because EDM is a non-contact process, it induces no mechanical stress into the component. Parts can be machined after heat treatment, eliminating the distortion risk of hardening a finished part, and delicate or thin-walled features survive machining untouched. That is why EDM sits at the heart of our die, mould and press-tool work, and why toolmakers trust it for the components that everything else depends on.
Share your drawings or specifications and we'll come back with a manufacturing approach, timeline and quote.
Request a Quote